Case Study
Custom Conveyor Locks Brazing Paste Timing at 120 PPM Across 8 Ring Terminal Variants
A terminal manufacturer needed every copper ring terminal past a sensor at exactly the same velocity. Bellco took the parts out of the vibratory environment and onto a dual-belt conveyor built in house.
The Challenge
A precision electrical terminal manufacturer came to Bellco with a request that pushed beyond standard parts feeding. Their line dispenses brazing paste — a precise dot of metal-filled compound — onto copper ring terminals as they travel toward a brazing furnace. The timing has to be exact: too early and the paste smears, too late and it misses the part entirely. The dispenser fires on a sensor signal, which means the part has to travel past that sensor at a precisely controlled velocity, every single time.
Standard bowl-to-track feeding couldn't deliver that consistency. Vibratory tracks rely on part-to-part contact and friction, which means the trailing parts always travel slightly slower than the leading ones. At 120 parts per minute — the speed the customer's brazing line required — that variance becomes the difference between a good braze and a rejected part.
Adding to the complexity: the system had to handle eight different ring terminal variants — different sizes, different barrel diameters, different overall lengths. Whatever Bellco built had to feed all eight without retooling, without recalibrating the paste dispenser, and without slowing down the line.
The Solution
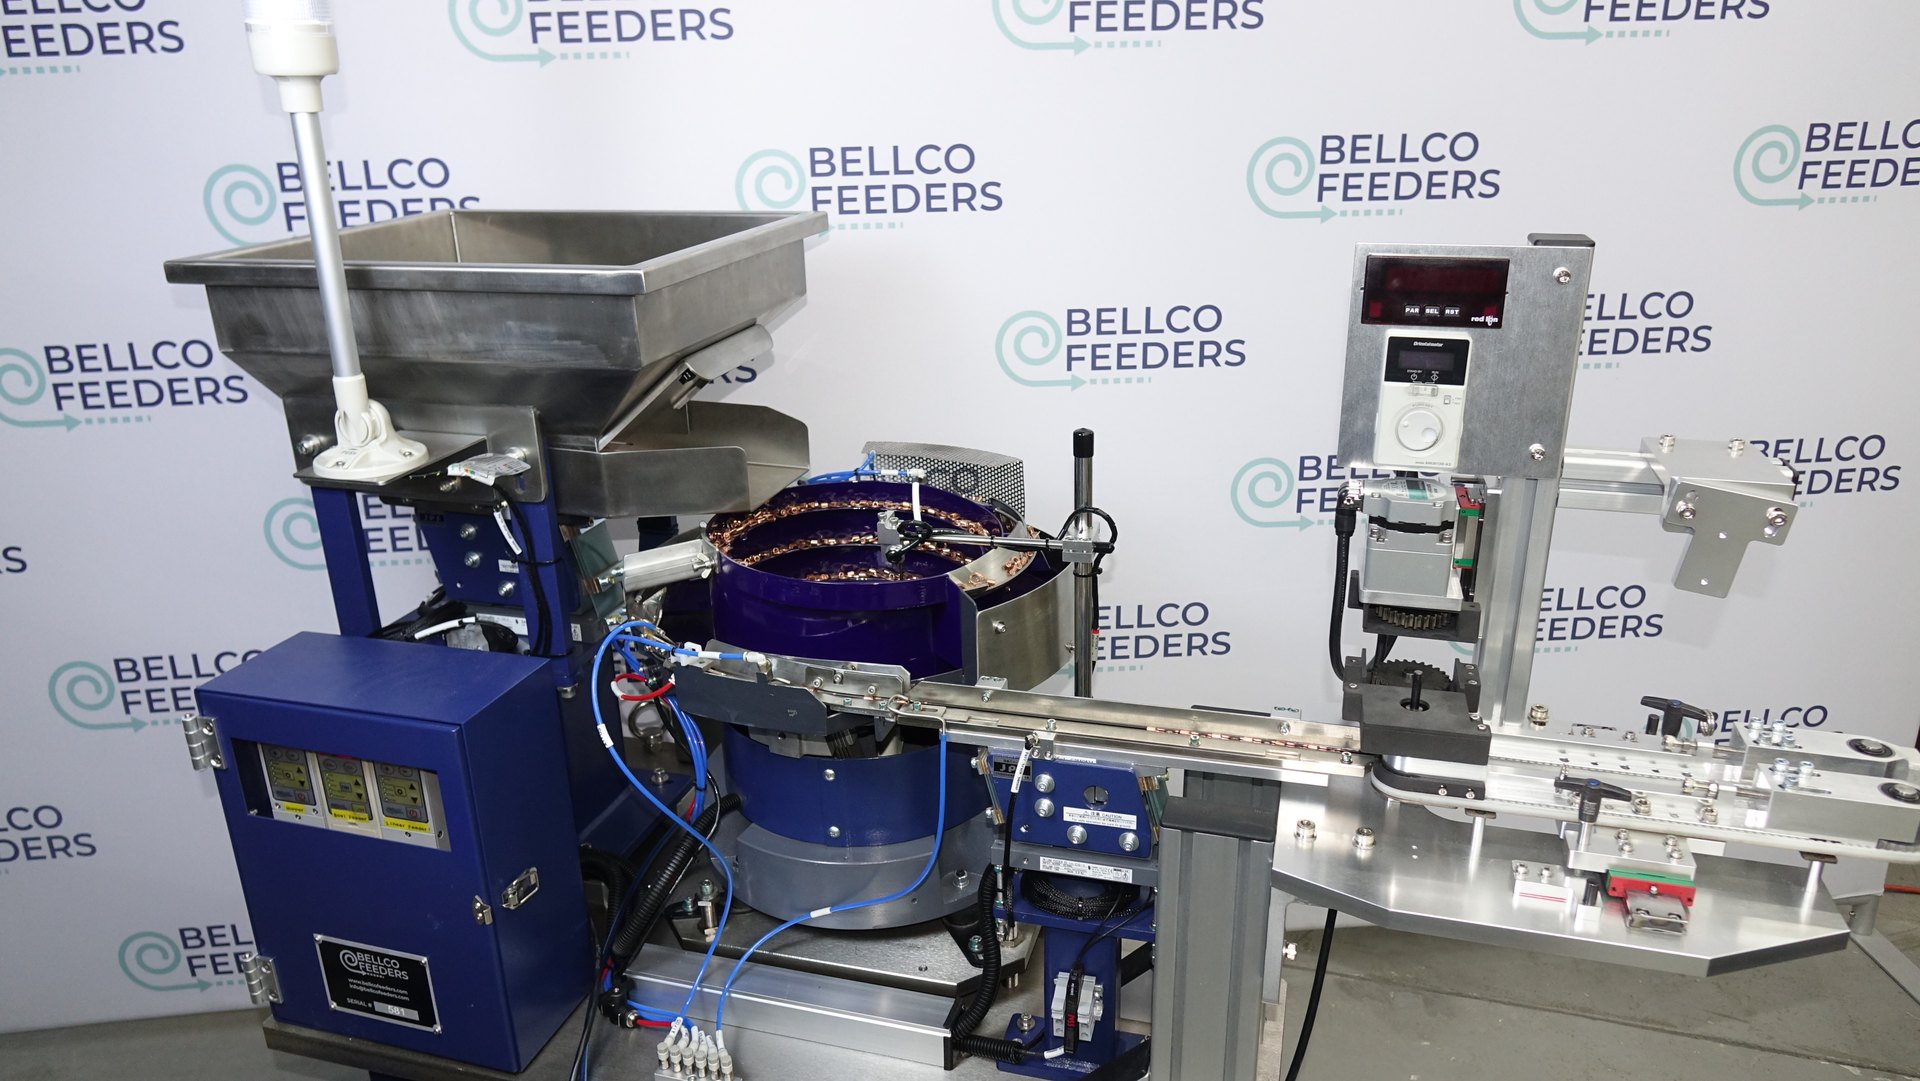
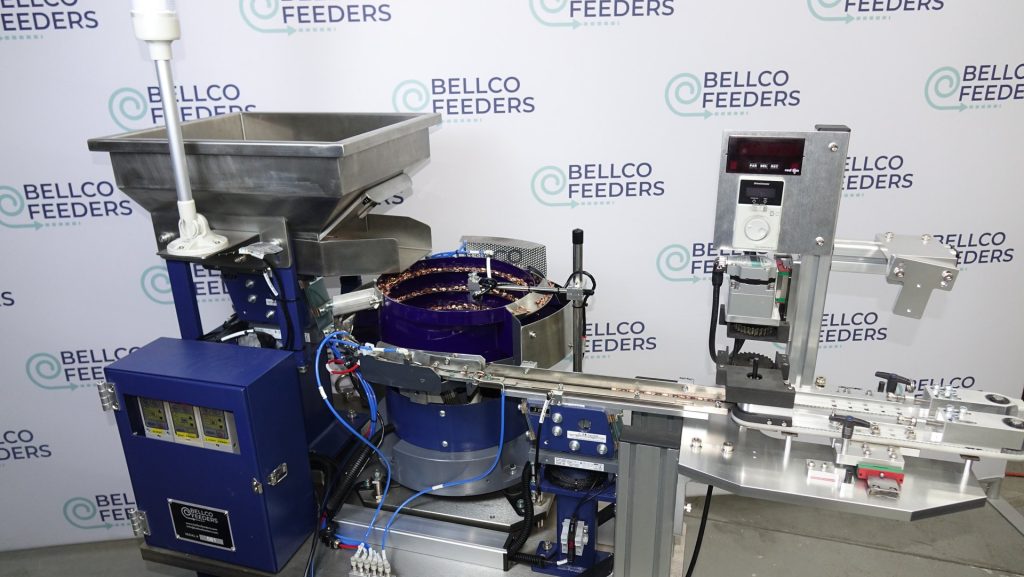
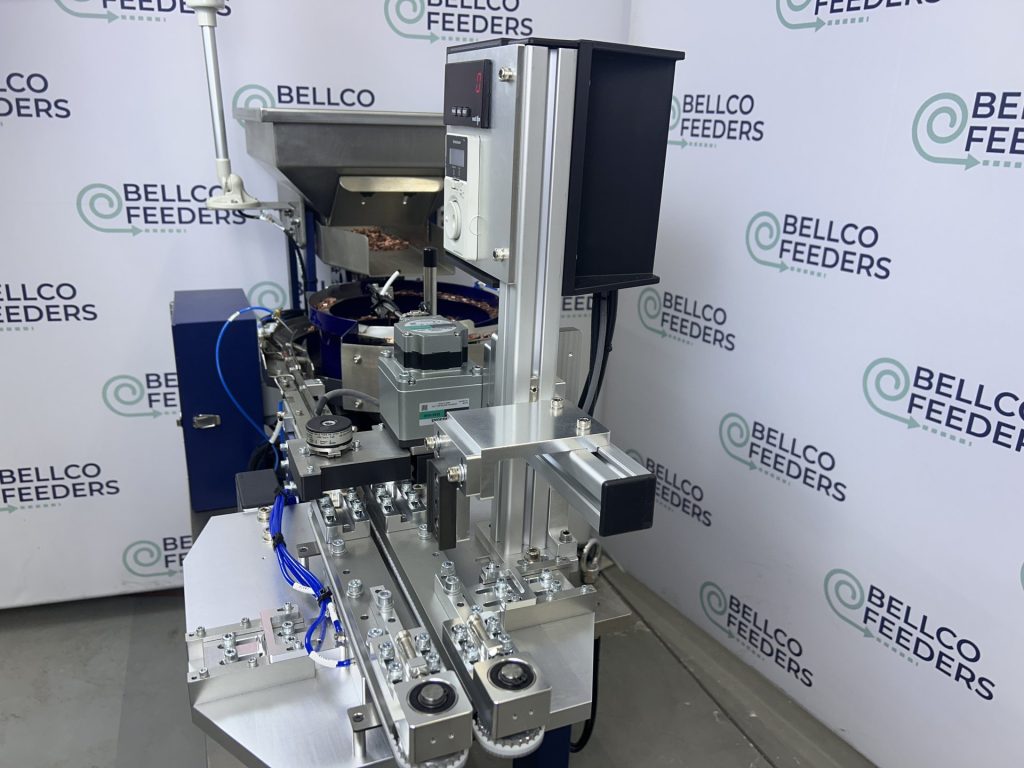
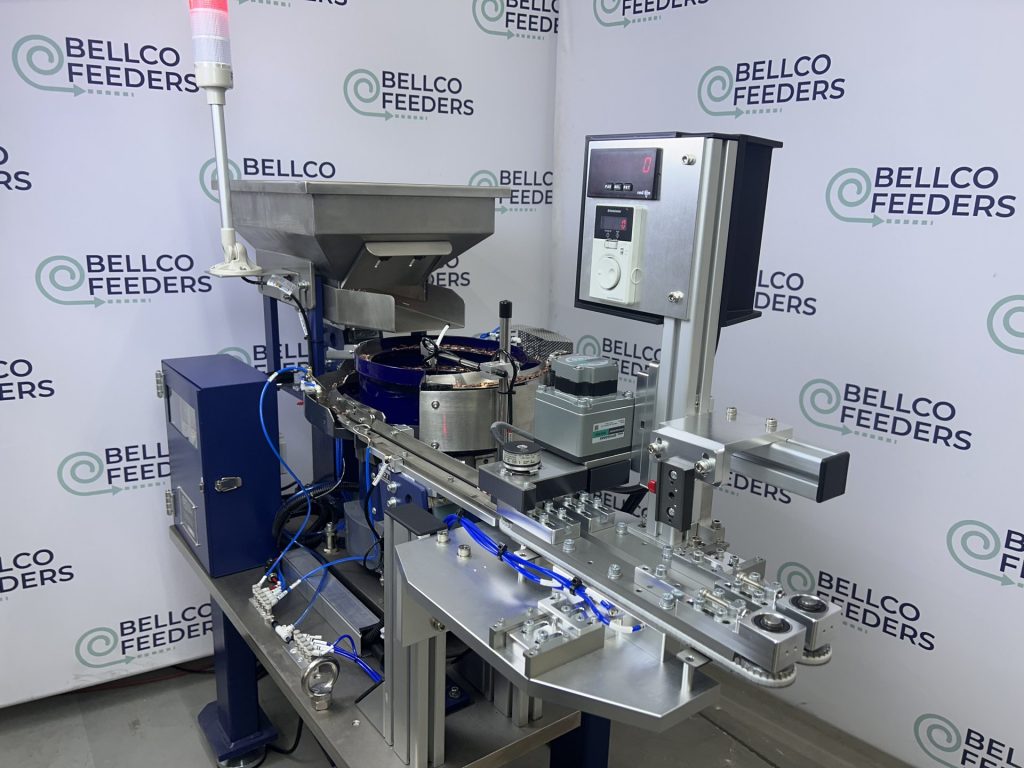
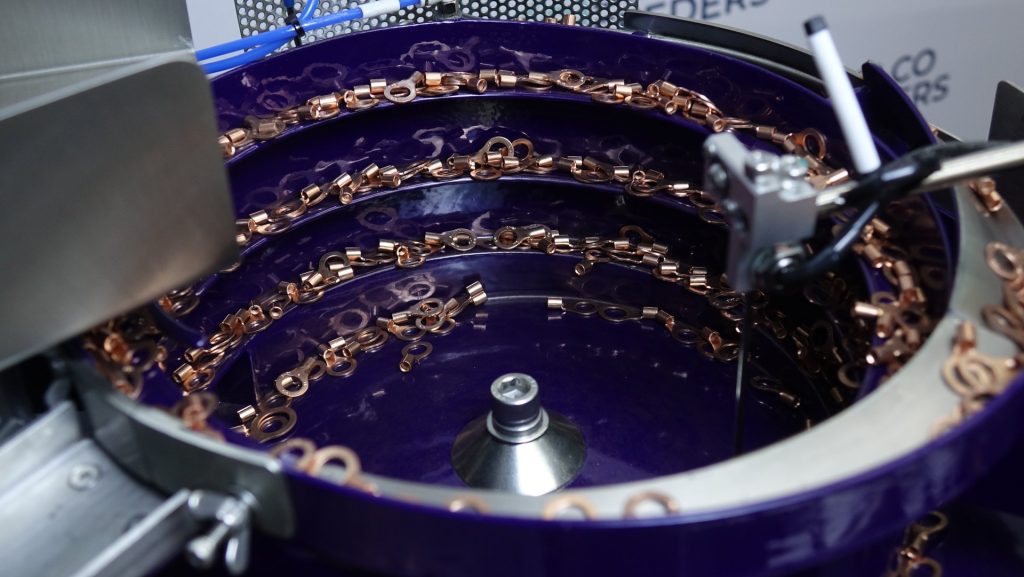
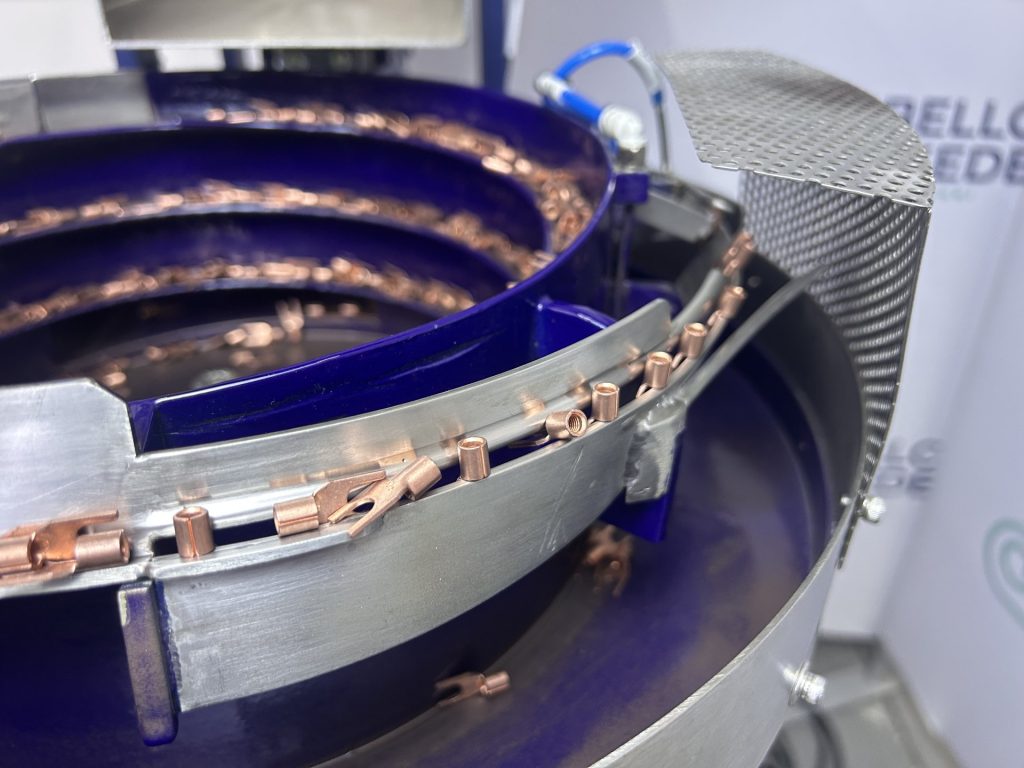
Bellco's answer was to take the parts out of the vibratory environment entirely once they reached the brazing zone. A 500mm vibratory bowl with polyurethane coating gently orients the copper terminals barrel-trailing and feeds them down a 355mm flat linear track. From there, the parts transition onto a fully custom dual-belt conveyor — designed and built entirely by the Bellco engineering team.
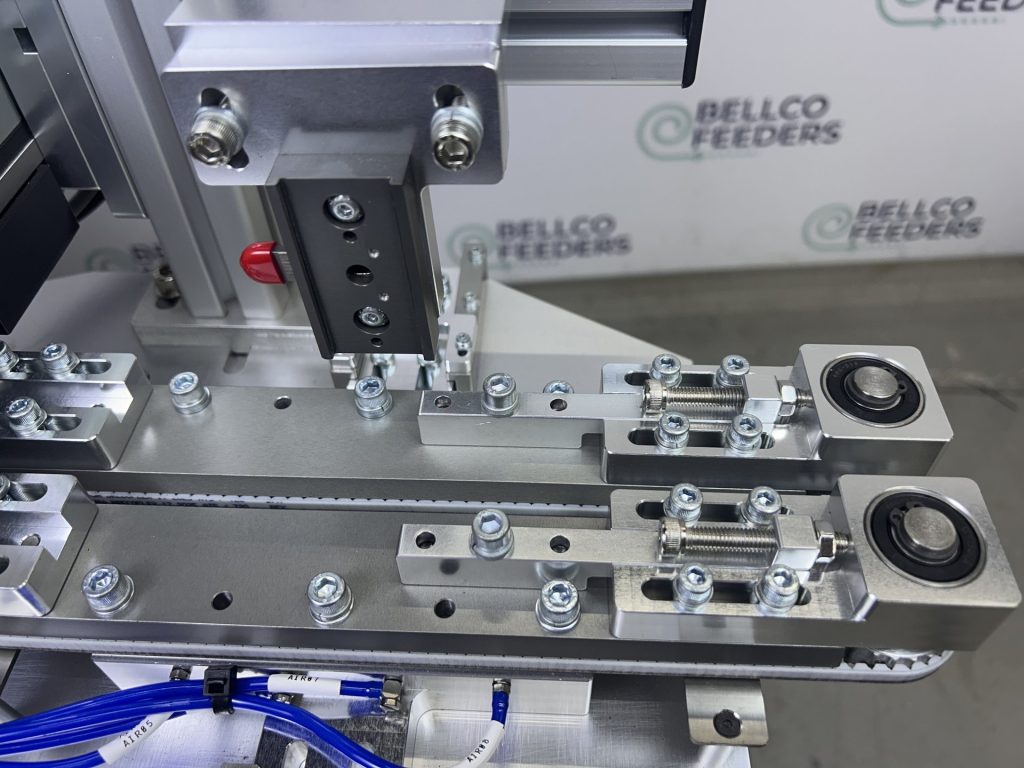
The conveyor is the engineering centerpiece. Two belts run in parallel along both sides of the part, gripping each terminal gently as it travels. Because the belts move at a fixed, motor-controlled velocity — not part-to-part friction — every terminal travels at exactly the same speed regardless of variant, regardless of part queue length. The customer's sensor and paste dispenser are mounted above the conveyor on a Bellco-built bracket with up, down, left, right and rotate adjustability, so the entire dispense zone can be dialed in for each part variant during commissioning.
Every component of the conveyor — bearings, belt tension, drive pulleys, side-rail geometry, transition from the vibratory track — was modeled in SolidWorks before fabrication. The complete 3D model was shared with the customer for approval prior to the build, so when the system arrived at their facility, the integration with their existing brazing line was already verified on paper.
Speed Control That Doesn't Compromise
The reason this system works at 120 PPM is the same reason most custom conveyor designs fail: details that don't show up until you build them. Belt tension calibrated to grip the smallest terminal variant without crushing the largest. Drive ratios tuned so the conveyor speed matches the bowl outfeed exactly, with no backup at the transition. Side-rail spacing engineered to accommodate variant geometry without retooling. Every piece of the design was solved in SolidWorks before the first piece of metal was cut — because at 120 parts per minute, there's no room to debug in the field.
Full System Overview
- 500mm vibratory bowl, 304 stainless steel with polyurethane coating, CW or CCW rotation
- 60–120 PPM feed rate, engineered to top end
- Barrel-trailing orientation, 355mm flat linear track outfeed
- Fully custom dual-belt conveyor designed and fabricated by Bellco
- Side-gripping belt design for precise, repeatable speed control across all 8 part variants
- Customer paste dispenser mounted on Bellco-built bracket with up, down, left, right and rotate adjustability
- Sensor-triggered paste dispense, fully I/O integrated with the customer's equipment
- 30-minute vibratory hopper with Keyence shortage sensor and full stopping function
- CUH variable-frequency digital controllers (PNP), housed in a lockable control box
- SMC pneumatics throughout, 110V or 220V power options
- 23mm ground steel nickel-plated baseplate on 4 welded steel legs, adjustable 30–45" leveling feet
- Fully designed and modeled in SolidWorks — complete 3D model shared with customer for approval before build
The Build
Have a similar project in mind?
Send us the part, the rate, and what has to happen to it downstream. An engineer will come back inside five business days.